Vacuum Pumps in the Pharmaceutical Industry

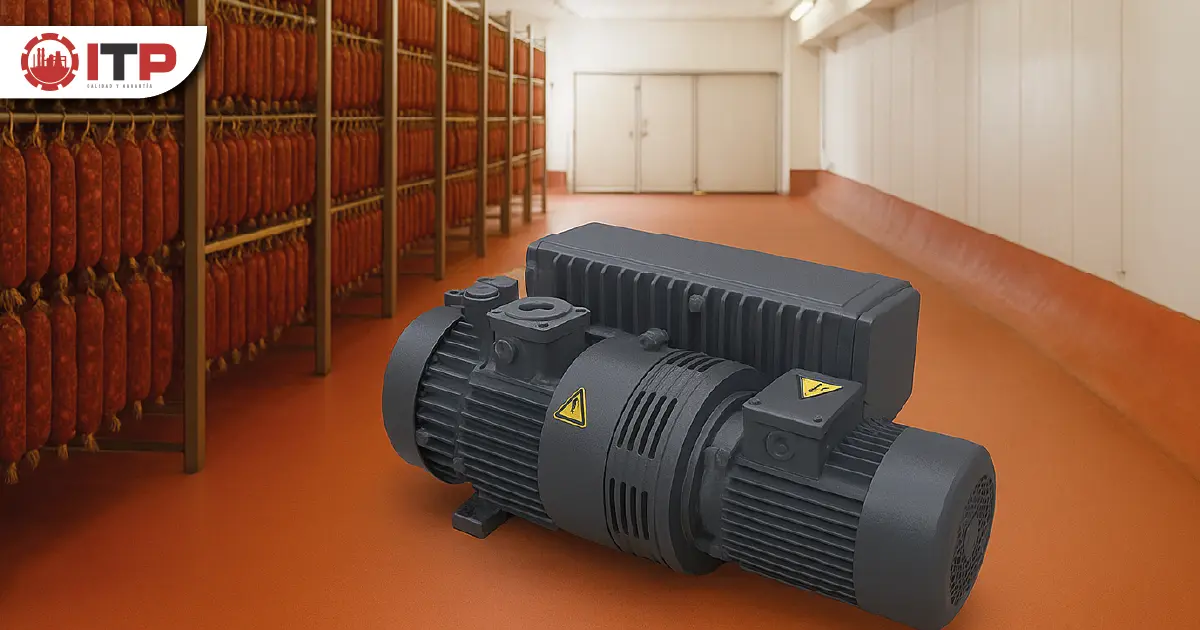
The pharmaceutical industry demands the highest standards of quality, precision, and safety. Every stage from drug production to packaging and storage relies on efficient and reliable equipment. Vacuum pumps play a crucial role in these processes by enabling gas removal, lyophilization, sterile filtration, and vacuum packaging of sensitive pharmaceutical products.
Using high-performance vacuum pumps ensures operational continuity and product integrity. Optimizing their performance is key to increasing productivity, reducing operational costs, and maintaining consistent product quality.
The Importance of Performance in Pharmaceutical Processes
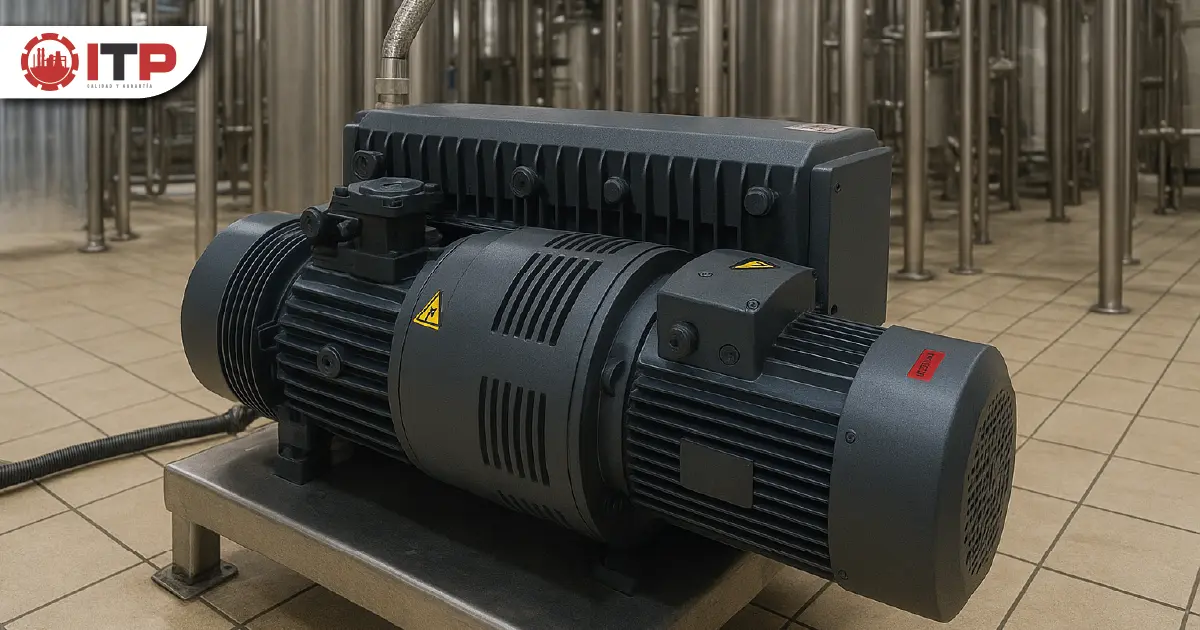
The performance of a vacuum pump directly impacts the efficiency and quality of pharmaceutical operations.
For instance, in lyophilization (freeze-drying) a critical process for vaccines and biologics the suction capacity and vacuum stability determine the uniformity and reliability of the final product.
Similarly, during vacuum packaging of tablets and capsules, an efficient vacuum pump prevents contamination and ensures airtight sealing. High-performance systems enable faster and more reliable production cycles, improving throughput without compromising quality.
Durability: The Key to Continuous Operation
Durability is a crucial factor for vacuum pumps in the pharmaceutical environment. These systems operate under tightly controlled conditions, where even minor contamination or equipment failure can result in significant product losses
To avoid this, pumps must be constructed from corrosion-resistant materials, equipped with high-grade seals, and include advanced filtration systems to maintain particle-free, contaminant-free performance.
Implementing preventive maintenance and continuous performance monitoring helps extend equipment lifespan and minimize downtime. The combination of durability and high performance ensures that critical processes such as lyophilization, vacuum distillation, or sterile packaging remain uninterrupted.
Technology and Automation for Greater Efficiency
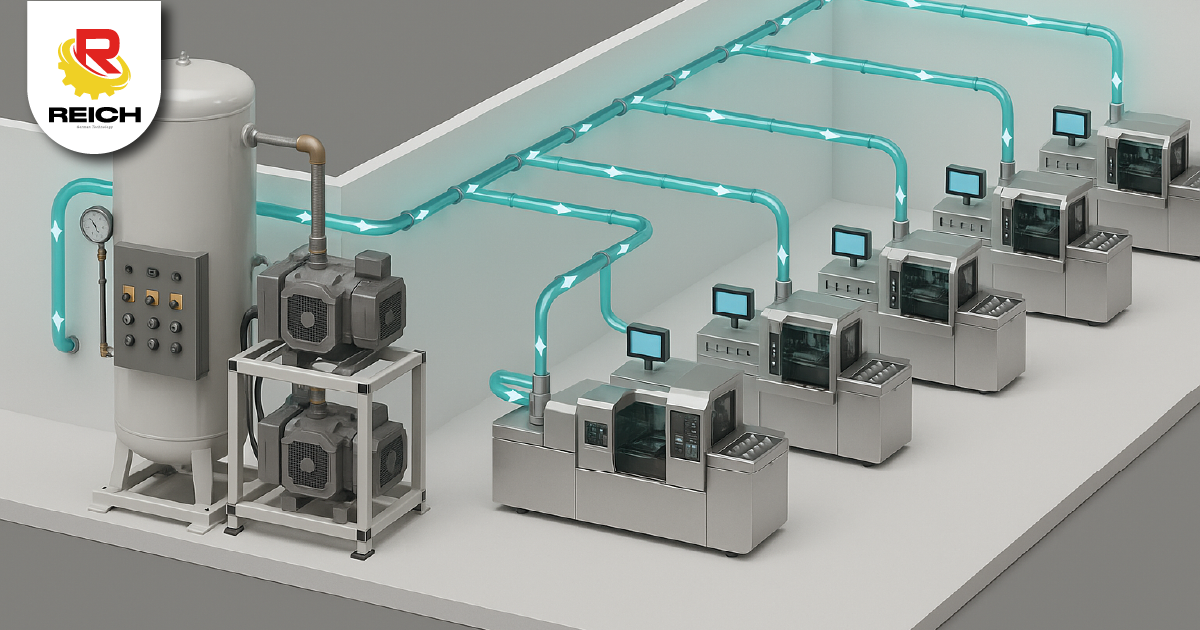
Modern vacuum pumps now integrate advanced technologies that enable real-time monitoring and automated control of every stage in the pharmaceutical process. Pressure sensors, smart control systems, and performance logs optimize plant operations and guarantee consistent, safe results.
Automation not only enhances energy efficiency, but also allows operators to detect anomalies early, ensuring both product quality and personnel safety.
Investing in high-performance and durable vacuum pumps is essential for any pharmaceutical plant seeking to optimize processes, ensure product safety, and comply with international regulations.
Combining reliable technology, preventive maintenance, and continuous monitoring ensures optimal performance improving productivity and minimizing operational risks. Vacuum pumps are not just another piece of equipment; they are strategic allies that guarantee efficiency, safety, and quality in pharmaceutical manufacturing.